|
|
August 2nd, 2014
 Brux Barrels, based in Lodi, Wisconsin, has earned a reputation for producing great-shooting tubes. Brux-made barrels have won their fair share of matches, and set some notable records in the process. Last year, Rodney Wagner shot the smallest five-shot, 600-yard group (.0349″) in the history of rifle competition, using a Brux barrel chambered for the 6mm Dasher.
Folks often ask us why Brux barrels shoot so well. “What’s the secret?” they ask. We can only answer with what Brux explains on its own website: “To make a cut-rifled barrel you have to start off with the proper ingredients: the best steel available, skill, and experience. Since there are really only two main suppliers of barrel-quality steel, the skill and experience is what really makes a barrel maker stand out.” Here is how Brux’s co-owners, Norman Brux and Ken Liebetrau, explain all the procedures involved in making a Brux cut-rifled barrel:
| Brux Barrel-Making Process, Start to Finish
We start out with either 4150 chrome-moly or 416R stainless steel double stress-relieved bar stock. The bar stock starts out at 1-9/32″ in diameter and 20-24 feet long so we cut it to length.
Step two is to rough-contour the outside of the barrel blank in a lathe.
Thirdly, the blank gets mounted into a Barnes gun drill. The cutter bit has holes through which oil or coolant is injected under pressure to allow the evacuation of chips formed during the cutting process. This is called “oil-through” or “coolant-through”. Without this, you wouldn’t want to even attempt drilling a hole 30” long and under ¼” in diameter. The combination of a 3600rpm and good flushing allows us to drill a beautifully straight and centered hole .005” under “land” diameter at a rate of 1” per minute.
Clean the barrel.
Next the blank is sent back to the lathe to machine the finished contour of the outside.
Clean the barrel again.
Now, the blank is sent on to the Pratt & Whitney reamer in which an “oil through” reaming tool is used to cut away the extra .005” left in the drilling process. The reamer makes an extremely accurate bore size and after it is finished the bore will have a better surface finish and will be at the proper “land” diameter.
Clean the barrel again.
In the sixth step we hand lap each barrel to remove any slight tool marks that may have been left by the reamer and inspect every one with a bore scope. If the barrel doesn’t meet our standards for surface finish and tolerance it doesn’t get any further.
Clean the barrel again.
The barrels then go onto the rifling machine which is responsible for cutting the all so familiar grooves in the bore. A caliber/land configuration-specific rifling head is used to progressively shave away small amounts of steel to form the rifling grooves. This is accomplished by simultaneously pulling the rifling head through the reamed blank as the blank is spun at a controlled rate. After each cut, the blank is rotated 90 degrees (for a four-land configuration) and after one full rotation (360 degrees) the rifling head is slightly raised to shave off the next bit of material. This process is repeated until we reach groove diameter.
Clean the barrel again.
Lastly, the barrel is hand-lapped again (to ensure a smooth bore), and a final inspection is performed with the bore scope.
The barrel is cleaned one last time, wrapped, packed, and shipped to [the customer]. |
Anyone reading this detailed description of the Brux barrel-making process will doubtless come away with a new appreciation for the time, effort, and dedication required to produce a premium match-grade cut-rifled barrel. Obviously, there are no easy shortcuts and great attention to detail is required each step of the way. As shooters we’re lucky that we have barrel-makers so dedicated to their craft.
Credit James Mock for steering us to this Barrel Making 101 feature on the Brux website.
August 2nd, 2014
by Lars Dalseide for NRABlog.com
There are five days in the NRA’s National Long Range High Power Rifle Championship. Five days of firing round after round at 6’ by 6’ targets up to 1,000 yards away. Five days of Camp Perry’s wind bouncing off Lake Erie while the sun fights to break through the occasional cloud.
This report was filed on Friday, August 1, 2014. CLICK HERE for the latest results.

Two sets of relays have already taken their respective Shooter Shuttles out to the pits, home of those 6’ by 6’ targets. There competitors take their turn at lifting and lowering the behemoth squares with every shot. Once fired upon, the target is lowered, scored, and raised back into place.

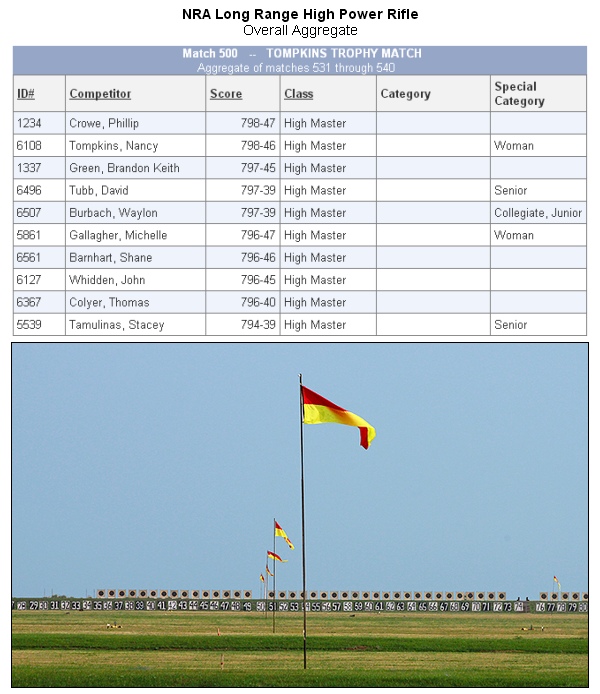
[As of Friday morning], only one round of relays is in the score books. Already, this is shaping up as a tightly-fought match. Only one point (and X-count) separates the top five shooters. Philip Crowe is currently in first with 798-47X. Just one X back, at 798-46X, is past champion Nancy Tompkins. A point behind Nancy are USAMU Shooter SSG Brandon Green, the legendary David Tubb, and Waylon Burbach. Nancy’s daughter Michelle Gallagher is in sixth. The other “Gallagher Girl”, SSG Sherri Jo Gallagher (below) is also competing this year.

CLICK HERE for Latest 2014 Long Range National Championship Results.
Photos courtesy NRABlog.com.
August 1st, 2014
At the 2014 National High Power Championships, Joe Hendricks recorded an inspirational come-from-behind victory that will long be remembered. But during this year’s competition, a 10-time past champion was noticeably absent from the firing line at Camp Perry. “Where’s Carl?” was the question many asked as the High Power Championships began.
Health concerns kept Carl Bernosky from competing at Camp Perry this year — serious health concerns. In fact, Carl is scheduled for back surgery today to deal with chronic pain and related neuro-muscular issues. Carl tells us: “I have had back problems for years but this March my bulging discs and sciatica flared with a vengeance. It was a very difficult time. It made functioning even with everyday tasks hard and shooting impossible. If you include something in your Bulletin please make sure that my friends and shooting competitors know how much I appreciate their kind words, thoughts and prayers. Thank you for thinking of me and hopefully I’ll be back on my feet soon. Please don’t let this in anyway overshadow Joe Hendricks’s well-deserved Championship. Joe shot superbly and I congratulate him on a great performance.”

We know that our Daily Bulletin readers wish Carl well and send their hopes that the surgery is 100% successful and that the healing process goes well. We all want to see Carl pain-free and back on the firing line. Carl is a great marksman — one of the best ever — and an equally great human being. We echo what one of his friends posted yesterday: “Carl is an absolute class act… humble, gracious, and a true gentleman. Heal up fast, Carl.”
In this exclusive interview filmed earlier this year (at SHOT Show), Carl talks about his approach to competition, and Carl offers helpful advice for fellow High Power competitors.
August 1st, 2014
 Have you got an old “Leapers” scope or other not-so-great optic that you’re embarrassed to mount on a rifle? Well now you can turn that ugly old optic into real money — two hundred dollars to be precise. Leica just announced a trade-in offer that provides a serious incentive to unload an old scope you don’t want or use. No broken scopes please — to qualify as a trade-in, the old scope much be functional with no broken parts. Here’s how the trade-in program works…
When you purchase a new Leica ER i riflescope from any authorized North American Leica dealer, you can receive $200.00 cash back by simply trading in a functioning riflescope of any make or model. Purchase your scope and send your trade-in to Leica between August 1 and October 31, 2014, to receive $200 by mail. The Leica ER i comes in two models: 2.5-10x42mm and 3-12x50mm. Both are available in three reticle configurations: Classic L4-A, Ballistic, and IBS.
To qualify to receive the $200 cash back, you must fill out Leica’s Trade-in Form and mail it to Leica along with your functioning trade-in scope. You must also include:
1. Copy of the sales receipt for the new Leica ER i scope.
2. Completed original ER i warranty registration

There is no brand or price limit on the trade-in. Leica will accept any brand, make or model of trade-in scope, so long as it is “functional” and a clear image and reticle are visible through the scope.
In fact, you might even find a new scope for less than twenty bucks. We found a Tasco 4x15mm scope on sale at MidwayUSA for just $9.99. And — get this — Midway is even offering free shipping on this item with orders of $25.00 or more. So if you and your buddies buy a total of three scopes (as one order) you can get them all delivered for free! CLICK HERE for $9.99 Tasco.

With this Tasco, you can shell out whopping $9.99 for a qualifying trade-in scope, and save $200.00 on a life-time guaranteed Leica. That’s smart shopping.
August 1st, 2014
We first featured this amazing stock last year. We felt this creation was such a stunning piece of work that it deserved a second look. If you missed this masterpiece the first time around, feast your eyes…
Sebastian (“Seb”) Lambang, creator of the SEB Coaxial Rests and the Coaxial Joystick Bipod, has engineered an impressive new wood and aluminum F-Class stock. The stock features a long, box-section aluminum fore-end with a wood rear section and wood-trimmed “wings” on the front bag-rider. The aluminum fore-arm has “buick vents” for weight reduction. From the end of the action rearward, the stock is mostly wood, with light and dark fancy wood laminates on opposite sides (left and right).
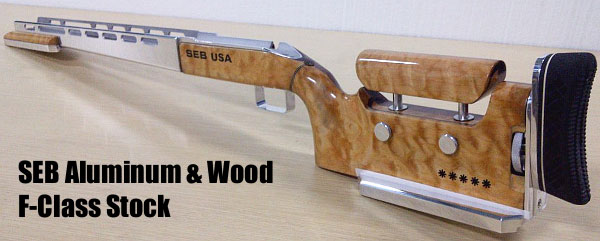

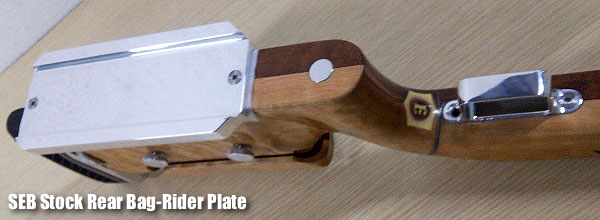
The foot of the buttstock has a very wide aluminum rear bag-rider with rails. The rear wood section appears to be two solid pieces of wood — but that is deceiving. Seb explains: “To save weight, the buttstock is hollow (using thin-walled wood)”. To strengthen the construction, Seb added carbon fiber inside the buttstock. So what you see is a wood outer shell with carbon fiber layers on the inside. The stock sports vertically-adjustable cheek-piece and buttplate. The thick, rubber buttpad should diminish felt recoil even when shooting big cartridges with heavy bullets.


This is an interesting, innovative stock design. And as with everything Seb produces, the craftsmanship, fit and finish are superb. We may get a chance to see how well this new stock shoots at the F-Class World Championships later this month in Raton, New Mexico.
Seb also crafted a handsome set of angled scope rails with beautifully-machined scope rings. Imagine being able to custom-make one-off products of this quality in your own machine shop!

July 31st, 2014
Glock, Inc. has contributed $50,000 to the Civilian Marksmanship Program (CMP) in support of the new CMP Marksmanship Park, in Talladega County, Alabama. Glock has pledged $150,000 total to be delivered in three, annual donations. The initial payment of $50,000 was presented by Glock’s Bob Radecki to Orest Michaels, CMP chief operating officer, who stated: “We are pleased that GLOCK has stepped up with [its] support of our park, which will be the most progressive public shooting venue of its kind in the United States.”

Glock’s dollars should help the CMP Talledaga Marksmanship Park construction plan stay on schedule. The Talladega facility is projected to open in May, 2015. The first CMP Southern Games event is planned for June 2015. Potentially, a second Southern Games event will be held in December 2015. The CMP’s new shooting complex is situated in the rolling hills of Talladega County, approximately two miles from the Talladega Super Speedway.
Electronic Targets for High Power Shooters
The new CMP Marksmanship Park will feature a 54-lane High Power rifle range with electronic targets at 200, 300, and 600 yards, plus an all-electronic scoring 100-yard sight-in rifle range with 50 firing points. With its electronic targets, the Talladega Parks will be one of the most advanced shooting complexes in the Western Hemisphere.
The High Power ranges will be equipped with state-of-the-art, all-weather electronic targets.

For handgunners, the new Talladega Park will feature a 50-yard pistol range, three 50-yard action pistol bays, twelve 25-yard action pistol bays and a 50-foot pistol range. A portion of the pistol complex will employ electronic targets. For shotgunners, CMP Talladega will offer a 15-station sporting clays course and a trap field with a five-stand overlay.
An aerial view shows the trees that will serve as natural dividers between each range.

July 31st, 2014
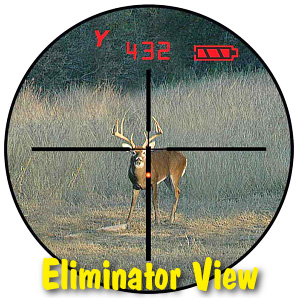 Burris Optics is currently offering significant rebates on three lines of scopes. You can get up to $100.00 in rebates on Burris Tactical and Fullfield II scopes. For the innovative Eliminator optics with built-in laser rangefinders, the savings are even bigger — you can get up to $200.00 in rebates with your purchase. We like the Eliminator scopes for Varmint hunting. The built-in rangefinder instantly calculates the needed hold-over, based on the target distance. Then the scope displays the corrected aim point as a red dot on the vertical cross-hair. Just put the red dot on your target and pull the trigger. The Eliminator does all the work for you — no turret clicking needed.
CLICK HERE for Burris REBATE Details and Forms

Rebate Instructions
These Burris products are available now at Grafs.com. Rebates available for purchases made between July 1, 2014 and December 31, 2014. Mail-in form must be signed, dated, and post-marked by January 31, 2015. View Full Offer Details.

July 30th, 2014
Story Based on Report by Kyle Jillson for NRABlog.com
Joseph Hendricks won the 2014 NRA High Power Rifle Championship with a 1789-76X Score. Hendricks topped a large field of 288 total competitors. In second place, two points behind, was past champion Norm Houle with 1787-85X. Defending 2013 High Power Champion SSG Brandon Green was a close third, with 1786-89X. Green had the high X-Count for the match. The top “Any Sights” competitor was Kenneth Lankford, whose 1780-76X was the eighth-highest total overall.

Great Shooting Takes Hendricks from Fifth to First on Final Day
Dawn on the final day of the 2014 NRA High Power Rifle Championship saw Joe Hendricks sitting in fifth place. But by sundown the Team Remington shooter had become the national champion. What happened in between was a shining example of consistency and perseverance.
Hendricks started the final day (Tuesday) four points down of the leader, tied for third but with a low X-Count. “I assumed everybody would go clean … so I needed to go clean just to maintain my spot,” Hendricks said. And clean he went. All 60 of Joe’s shots on Tuesday fell within the 10-ring. In fact, he hit straight 10s for the last 100 shots of the 180-shot championship. That is an impressive feat.

Three Generations of Hendricks on the Firing Line
Hendricks has the unique privilege to shoot with his son, Joe Hendricks, Jr., and his father, Gary Hendricks. The rest of his family was there to cheer him on as well.
Altered Course of Fire on Final Day
Tuesday’s matches followed an unusual break after severe winds on Monday caused a complete cancellation of the matches. Normally, on the final day of the High Power Championship, competitors shoot matches at 200, 300, and 600 yards. This year, due to the Monday cancellation, competitors did not fire a 200-yard match, but instead fired the 300-yard match and TWO 600-yard matches.
View Photos from 2014 High Power Championships
When everyone found themselves back on the firing line Tuesday morning, the wind had died down. “The winds weren’t too tricky. I shot two nice groups at 300. Not the X-count I wanted, but I got all the points,” Hendricks explained. “When I got back to 600 I just tried to do the same thing. The wind dropped off enough a couple times that if I shot I’d lose points, so I waited until it came back.”
Hendricks finished with 1789-76X, two points ahead of Norman Houle (1787-85X), a three-time High Power National Champion. In third place, with 1786-89X, was SSG Brandon Green, last year’s High Power Rifle Champion.
July 30th, 2014
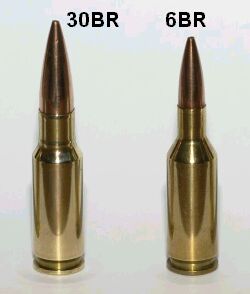 The 30BR is an amazing little cartridge. However, 30BR shooters do have to neck-up 6mmBR brass and then deal with some issues that can arise from the expansion process. One of our Forum members was concerned about the donut that can form at the new (expanded) neck-shoulder junction. Respected bullet-maker Randy Robinett offers tips on how to deal with the “dreaded donut”.
The Forum member was concerned about thinning the brass if he turned his 30BR necks after expansion: “Everything I have found on 30BR case-forming says to simply turn off the bulge at the base of the neck caused by the old 6BR shoulder. I expanded my first case and measured the neck at 0.329″ except on the donut, where it measures 0.335″. Looking inside the case… reveals a groove inside the case under the donut. Now, it is a fact that when I turn that neck and remove the donut, the groove is still going to be there on the inside? That means there is now a thin-spot ring at the base of the neck that is .005 thinner than the rest of the neck. Has anyone experienced a neck cracking on this ring?”
Randy Robinett, who runs BIB Bullet Co., is one of the “founding fathers” of the 30BR who help prove and popularize the 30 BR for benchrest score shooting. Randy offers this advice on 30BR case-forming:
While the thinner neck-base was one of our original concerns, unless one cuts too deeply INTO the shoulder, it is not a problem. For my original 30BR chamber, thirty (30) cases were used to fire 6,400 rounds through the barrel. The cases were never annealed, yet there were ZERO case failures, neck separations, or splits. The case-necks were turned for a loaded-round neck diameter of .328″, and, from the beginning, sized with a .324″ neck-bushing.
The best method for avoiding the ‘bulge’ is to fire-form prior to neck-turning (several methods are successfully employed). Cutting too deeply into the shoulder can result in case-neck separations. I have witnessed this, but, with several barrels and thousands to shots fired, have not [personally] experienced it. The last registered BR event fired using that original barrel produced a 500-27x score and a second-place finish. [That’s] not bad for 6K plus shots, at something over 200 firings per case.
Check out the 30BR Cartridge Guide on AccurateShooter.com
You’ll find more information on 30BR Case-forming in our 30 BR Cartridge Guide. Here’s a short excerpt from that page — some tips provided by benchrest for score and HBR shooter Al Nyhus:
30BR Case-Forming Procedure by Al Nyhus
The 30BR cartridge is formed by necking-up 6BR or 7BR brass. You can do this in multiple stages or in one pass. Most of the top shooters prefer the single-pass method. You can use either an expander mandrel (like Joe Entrekin does), or a tapered button in a regular dies. Personally, I use a Redding tapered expander button, part number 16307. This expands the necks from 6mm to .30 cal in one pass. It works well as long as you lube the mandrel and the inside of the necks. I’ve also used the Sinclair expander body with a succession of larger mandrels, but this is a lot more work and the necks stay straighter with the Redding tapered button. This button can be used in any Redding die that has a large enough inside diameter to accept the BR case without any case-to-die contact.
Don’t be concerned about how straight the necks are before firing them the first time. When you whap them with around 50,000 psi, they will straighten out just fine! I recommend not seating the bullets into the lands for the first firing, provided there is an adequate light crush-fit of the case in the chamber. The Lapua cases will shorten from approx. 1.550″ to around 1.520″ after being necked up to 30-caliber I trim to 1.500″ with the (suggested) 1.520 length chambers. I don’t deburr the flash holes or uniform the primer pockets until after the first firing. I use a Ron Hoehn flash hole deburring tool that indexes on the primer pocket, not through the case mouth. — Al Nyhus
July 30th, 2014
Tonight, American Rifleman TV features the Bianchi Cup, one of the oldest, richest, and most prestigious pistol competitions on the planet. In 2014 over $500,000 in cash and prizes was up for grabs. That stellar pay-out (and the prestige of winning) attracts the world’s top pistoleros.

This Bianchi Cup event was founded in 1979 by former police officer and holster maker John Bianchi. Success in the Bianchi Cup requires a perfect balance of speed and accuracy. The 192-shot championship allows a maximum aggregate of 1920 points across four timed events: Practical, Barricade, Moving Target and Falling Plate. In addition to being grouped by age, gender, and shooting skill, competitors may opt to shoot in the Open, Metallic, or Production divisions.
Watch Preview of July 30 Episode of American Rifleman TV
This week’s episode also features a vintage Vickers belt-fed machine gun from World War I. You can view interesting segments from past American Rifleman TV episodes, along with “Gun of the Week” video reviews at AmericanRifleman.org/Videos:

|


