Forum member Skeeter has a 6mm Dasher falling block varmint rifle. The Dasher case is based on the 6mm BR Norma cartridge with the shoulder blown forward about 0.100″ and out to 40°. This gives the Dasher roughly 3.5 grains added capacity compared to the standard 6BR.
Last year, Skeeter needed to form 300 cases for varmint holiday. Skeeter decided to fire-form his brass without bullets. This method avoids barrel wear* and saves on components. There are various ways to do this, but Skeeter chose a method using pistol/shotgun powder, some tissue to hold the powder in place, Cream of Wheat filled to within an 1/8″ of top of the neck, and a “plug” of tissue paper to hold it all in place. Shown below are cases filled with a pistol/shotgun powder charge topped with Cream of Wheat and then a tissue paper plug.
To ensure the case headspaced firmly in his Dasher chamber, Skeeter created a “false shoulder” where the new neck-shoulder junction would be after fire-forming. After chamfering his case mouths, Skeeter necked up all his cases with a 0.257″ mandrel (one caliber oversized). Then he used a bushing neck-sizing die to bring the top half of the neck back down to 0.267″ to fit his 0.269″ chamber. The photo below shows how the false shoulder is created.
After creating the false shoulder, Skeeter chambered the cases in his rifle to ensure he could close the bolt and that he had a good “crush fit” on the false shoulder, ensuring proper headspace. All went well.
The next step was determining the optimal load of pistol powder. Among a variety of powders available, Skeeter chose Hodgdon Titewad as it is relatively inexpensive and burns clean. The goal was to find just the right amount of Titewad that would blow the shoulder forward sufficiently. Skeeter wanted to minimize the amount of powder used and work at a pressure that was safe for his falling block action.
Working incrementally, Skeeter started at 5.0 grains of Titewad, working up in 0.5 grain increments. As you can see, the 5.0 grain charge blew the shoulder forward, but left it a hemispherical shape. At about 7.0 grains of Titewad, the edge of the shoulder and case body was shaping up. Skeeter decided that 8.5 grains of Titewad was the “sweet spot”. He tried higher charges, but the shoulder didn’t really form up any better. It will take another firing or two, with a normal match load of rifle powder and a bullet seated, to really sharpen up the shoulders. Be sure to click on the “View Larger Image” link to get a good view of the cases.
The process proved to be a success. Skeeter now has hundreds of fire-formed Dasher cases and he hasn’t had to put one bullet through his nice, new match-grade barrel. The “bulletless” Cream of Wheat method allowed him to fire-form in a tight-necked barrel without neck-turning the brass first. The only step now remaining is to turn the newly Dasher-length necks down about .0025″ to fit his 0.269″ chamber. (To have no-turn necks he would need an 0.271″ or 0.272″ chamber).
Skeeter didn’t lose a single case: “As for the fire-forming loads, I had zero split cases and no signs of pressure in 325 cases fire-formed. Nor did I have any misfires or any that disbursed COW into the action of the firearm. So the COW method really worked out great for me and saved me a lot of money in powder and bullets.” To learn more about Skeeter’s fire-forming process, read this Dasher Fire-Forming Forum Thread.
*Skeeter did have a fire-forming barrel, but it was reamed with a .269 chamber like his 10-twist Krieger “good” barrel. If he fire-formed with bullets, he would have to turn all 300 necks to .267″ BEFORE fire-forming so that loaded rounds would fit in the chamber. Judging just how far to turn is problematic. There’s no need to turn the lower part of the neck that will eventually become shoulder–but how far down the neck to turn is the issue. By fire-forming without bullets now he only has to turn about half the original neck length, and he knows exactly how far to go.
Some High Power shooters on the Forum asked about carts for carrying their gear to the range. You can certainly purchase a factory-made, purpose-built cart that folds up and has all the bells and whistles. The Creedmoor Sports CRC-1 (photo right) is a proven, quality product that works great. You’ll find these used by top shooters at Camp Perry. But the Creedmoor CRC-1 cart costs $499.95.
For a tenth that price ($49.99), plus a few dollars more for do-it-yourself enhancements, you can have a heavy-duty cart that will haul all your gear just fine, though it doesn’t fold up.
Check out the Harbor Freight Welding Cart, item #65939. This cart is ON SALE right now for just $49.99. Overall size is 29-1/2″ L x 20″ W x 49″ H, and width between side rails is 18″. The wheels (with tires) are 20 3/4″ in diameter for smooth rolling. Consider that, if you made your own cart from scratch you could easily pay $30.00 or more just for the large-diameter wheels and axle. Do note — this cart has air-filled tires. Be sure to inflate before you go to the Range!
As sold, the Harbor Freight Welding Cart isn’t quite ready for range use. But it’s easy to add plastic side-panels on the bottom unit, and fit a barrel-holding system on the cross-tube. I also suggest bolting/welding on extra spacers on the most forward underside edge of the bottom so that, at rest, the cart tilts slightly back. This ensures rifles and gear won’t flop forward. (A bit of extra lift also keeps the bottom plate out of the dirt and gravel.)
How to Upgrade Welding Cart for Range Use
Get a block of hard foam rubber. Cut keyhole slots in the rubber to grip the barrel and umbrella/scope stands. Mount the rubber block to the cross piece with self-tapping screws, or drill a horizontal channel in the rubber so the whole block fits over the cross-tube. On the lowest leading edge of the welding cart box (at ground level, front), fit a block of wood 2″ high (you can also fabricate metal extensions). This will make the cart lean back a little more, which helps stabilize the contents on sloping terrain.
You’ll want to enclose the sides of the bottom box area so small items don’t fall out. You can tack-weld aluminum side-plates if you want a fancy appearance. I prefer to just cut sheet plastic from a home improvement store. These plastic panels can be attached with screws or even zip-ties around tubing.
Run the plastic side panels up high enough that stuff like hats and muffs don’t fall out. After transport you can transfer ammo boxes and small items to the upper box (attached to the back side of the cross-tube).
The hardest component to find may be the hard rubber blocks for the barrel keeper, but you can also make a barrel-holding block out of wood, with some carpet to protect the barrels. The nice thing about the rubber is that it can be cut to snap over the barrels so you don’t need straps. Likewise, you can drill a hole transversely through the rubber, then slot it from the bottom and it will slide over the horizontal tubing with no fasteners needed.
Comment: This cart is heavy and it takes up a lot of space. You’ll need a station wagon, SUV or pickup truck to haul it around. But it’s cheap. The money you save on a range cart could pay for a new Krieger or Bartlein barrel, AND some new brass. Those things (new barrel and brass) will likely improve your scores more than having a fancy $500.00 range cart.
Robert Whitley of AR-X Enterprises, LLC builds match-grade uppers for AR-platform rifles. Many of Robert’s favorite chamberings are based on the 6.5 Grendel case necked-down to 6mm. Until 2011, Lapua was the only source for 6.5 Grendel brass. As you’d expect, Lapua’s Grendel brass is truly excellent, but it is also pricey, and sometimes hard to find. Now Hornady is producing USA-made 6.5 Grendel brass. Robert Whitley has worked with the Hornady 6.5 Grendel brass for over a year now and he is able to assess its performance compared to the original Lapua version. Writing in our Shooters’ Forum, Robert reveals: “It’s decent brass but hot loads will loosen the primer pockets fast. With moderate loads you will get good case life and service from the brass and it can deliver excellent accuracy as well. Not Lapua but not bad either.”
Robert reports: “I was able to get my hands on some of Hornady’s 6.5 Grendel brass. My big question was how it would measure up, particularly the loaded necks, and whether it would be compatible with our existing 6mmAR and Turbo 40 die sets. As it turns out, this brass looks like a perfect fit for our existing die sets (and obviously 6.5 Grendel die sets too). Accordingly, folks with existing die sets will be able to use the Hornady brass without any issues.” However, as the loaded neck on the Hornady brass is .001″ (one-thousandth) slimmer than Lapua brass, you may want to try a smaller bushing when sizing Hornady Grendel brass.
The Hornady 6.5 Grendel brass has a LARGE Flash Hole, about .078″ versus .0591″ for Lapua brass. Dimensionally, the biggest difference is the shoulder diameter, with the Hornady brass measuring 0.428″ vs. 0.424″ for the Lapua brass. The Hornady is actually a better fit for 6mmAR chambers which are about 0.432″ at the shoulder. Interestingly, case H20 capacity is virtually identical. Water capacity of new, unfired Hornady 6.5 Grendel brass is 35.1 grains, while new, unfired Lapua Grendel brass holds 35.0 grains of H20. Both brands of Grendel brass increase to about 36.0 grains H20 capacity after firing and full-length sizing.
Here are some of the particulars of the Hornady cases:
Hornady 6.5 Grendel Brass
Lapua 6.5 Grendel Brass
Flash hole diameter: ~ .078″
OAL of brass: Average 1.515″
Weight of cases: 111.7 to 113.0 grains
Web diameter, unfired: 0.4375″
Shoulder diameter, unfired: 0.428″
Loaded neck diameter: 0.2895″
6mmAR loaded neck: 0.270″
Flash hole diameter: 1.5mm (0.0591″)
OAL of brass: Average 1.515″
Weight of cases: 111.0 to 112.5 grains
Web diameter, unfired: 0.4385″
Shoulder diameter, unfired: 0.424″
Loaded neck diameter: 0.290″
6mmAR loaded neck: 0.271″
Past F-Open Class National Champion (and Forum Member) Larry Bartholome, has authored an authoritative article on the 2011 F-Class National Championship held last fall in Lodi, Wisconsin. Larry writes: “With a wind tunnel for a range, and rain that canceled the final team match, only the strongest stood on the winners’ podium when the Championships ended”. Larry provides a day-by-day guide to the match, with complete results for both F-Open and F-TR classes. You’ll find Larry’s article in the February 2012 edition of Shooting Sports USA.
You can read, for FREE, the digital version of Shooting Sports USA. CLICK HERE to read Larry’s article (pp. 20-22). Along with the report on the F-Class Nationals, there are many other items of interest in the February edition of Shooting Sports USA. You’ll find a 14-page 2012 Event Calendar that covers NRA competitions all across the country.
In addition, this month’s edition features a well-written, 4-page Guide to Field Target Competition by Jock Elliot. Field Target is a form of outdoor silhouette shooting using high-tech PCP Air Rifles with high-magnification scope. Check out the special Marauder Hybrid bullpup used by Team Crosman member Ray Apelles in the photo below. These high-end rigs are not cheap. A “full-race” Open Class Field Target rifle can cost up to $3000.00 with another $1000.00-$3000.00 for optics.
Top Shot fans, mark you calendars. The fourth season of Top Shot on the History Channel begins in one week. The Season 4 premiere airs Tuesday, February 14 (Valentine’s Day) at 10:00 PM Eastern. The selection of firearms (and other weapons) should be even more interesting this season. And, with a bigger budget to play with, Top Shot’s producers are ramping up the level of challenges. Season 4 begins with the biggest twist in Top Shot history: two competitors are sent packing immediately after a surprise shoot-off in the opening minutes of the first episode. Later, two shooters get a taste of WWII combat as they fire an M1 Carbine from a motorcycle sidecar and attempt to stay in the game. Colby Donaldson returns as host.
Here are Video Profiles of Three Season 4 Competitors (others at link below):
Michelle Viscusi (U.S. Army Nat’l Guard MP, serving with the Border Patrol)
The NRA Competitive Shooting Department is promoting a trivia contest on its Facebook page. Once every couple of weeks, the Competitive Shooting staffers gather round, decide on a question and pick a prize. Correct answers are put in a hat and winner is picked.
The last winner, Pennsylvanian Robert Berl, correctly answered that Michelle Gallagher won the 1,000 yard Any Sight Match (Band of Brothers Match) at the 2010 National Long Range Championships.
If you submit a correct entry in this week’s contest, you can win a valuable prize. This week’s question is: “Who was the winner of the inaugural 1979 Bianchi Cup?” Once you’ve figured that out, send an email to compadmin@nrahq.org by 4:00 pm ET on Thursday, February 13 and you can win a 2011 MidwayUSA & NRA Bianchi Cup Gift bag. Inside the bag is a 2012 Bianchi Cup brochure signed by John Bianchi himself and 2011 Bianchi Woman’s Champion Jessie Harrison.
if you turn your case-necks, here’s a tool from 21st Century Shooting that can can save time, and help you produce better, more consistent turned necks. 21st Century’s Neck-Turning Lathe system, introduced last spring, may revolutionize the way reloaders turn their case necks. Watch the video and you’ll see why. If you’re never turned cases before, you may become a convert after seeing how quickly and easily the new 21st Century Neck-Turning Lathe does the job.
The mini-lathe has unique fittings on the left and right sides that allow both the case-holder and the neck-turning tool to float. As a result this tool maintains near-perfect concentricity during the cut. 21st Century’s John Perkins explains: “The floating design of the neck turner and the case driver allows the case mouth (bore) to run on the arbor absolutely concentric, therefore allowing O.D. to be turned concentric with I.D. The tailstock creates a horizontal inline support for the base of the case. This also allows the operator to keep both hands on the power screw driver or drill, making it very easy to control the feed rate and to produce a very fine, turned finish.” Having the system float at both ends was key, according to John: “By allowing both the turner and the case to float, everything self-aligns. This maintains concentricity and allows the unit to work with very low torque.”
Neck-Turning Lathe is Fast Yet Precise
Using power from a drill or electric screwdriver, this tool will turn necks fast — in a matter of a few seconds. And it produces beautiful, smooth necks that are extremely uniform. Tests show that the lathe, used with the 21st Century Neck-Turning Tool, will hold 0.0002 (two ten-thousandths) neck wall tolerances. And it will do that time after time.
Turn Necks in a Single Pass
Using traditional hand-methods, turning case necks can be time-consuming and fatiguing. Many folks will experience hand pain or cramping after just a dozen cases. Watch the video, you’ll see how fast and easy neck-turning can be with the new mini-lathe. You get an exceptionally good cut in seconds. Very importantly, with this system, you may be able to switch from a double-pass cut, to a single-pass cut. Yes, even if you’re making a deep cut, we think there is a good chance you can turn all your necks in a single pass. That can cut your labor time in half!
Why does the 21st Century Neck-Turning Tool cut so well? First, the Neck-Turning Tool employs ultra-sharp carbide cutters that are custom-ground to fit the shoulder angle of your cartridge. This allows you to make a perfect cut extending down the shoulder 1/32 of an inch. Second, the system aligns the case neck on the arbor (mandrel) so well, and the cutter is so sharp, that very little torque is required. This allows the cutting process to go very smoothly. The case-holder is also unique — it features a O-ring so it holds the case firmly in place without marring or bending the case head. The tailstock case-holder adjusts to accommodate cases from 17 Fireball to a .416 Rigby.
More Case Prep Tools for Lathe in Future
In the near future 21st Century will offer additional case prep attachments for the new mini-lathe. 21st Century plans to provide bullet-pointing system and other options. These will all work with the same lathe “chassis”, and will run with power. John states: “This is a modular system, all parts interchange. So if you have an existing 21st Century Shooting Neck Turning Tool or Bracket, everything will fit.”
The 21st Century Neck-Turning Lathe costs $245.00, complete with Neck-Turning Tool ($85.00 value) and one case-holder driver. The Neck-Turning Tool comes with a carbide cutter with user choice of shoulder angle (Arbors and Mandrels are sold separately). Perkins recommends using the Neck-Turning Lathe with power, but it will also work with an optional hand crank. NOTE: Currently the Neck-Turning Lathe works ONLY with the 21st Century Neck-Turner. It will not work with K&M, Sinclair, or Forster tools. But that’s not a real drawback because the 21st Century tool is certainly one of the best on the market today. You can purchase the Neck-Turning Lathe (complete with Neck-Turner and Case-Holder) through the 21st Century website, or call (260) 273-9909.
Disclosure: 21st Century Shooting advertises with AccurateShooter.com.
Polymer Injection Molding (PIM) of Monson, MA has been awarded U.S. Patent 68,062,736 for overmolding gunstocks coated with a decorative or protective substrate. Overmolding typically is used to enhance synthetic stocks by molding a soft, rubber-like material to gripped areas of a gunstock (fore-end and pistol grip). Sometimes overmolding is applied to the entire stock. Overmolding also is used to decorate stocks with contrasting colors and textures.
Applying overmolding to a decorated gunstock (camo, wood grain, etc.) has proven to be extremely difficult and costly and has not been practiced widely. As a result, overmolded stocks typically have a black, grey, tan or other basic, out-of-the-mold colors. See, e.g. the Hogue Over-Molded stocks. PIM’s patented technology changes all that. Now overmolding can be applied over camo-dipped and other patterned stocks. This is typically done in key contact areas on the fore-arm and on the pistol grip section.
According to PIM President Jim Ryan, “We did our first overmolded stock for a gun manufacturer over ten years ago. It wasn’t long before everybody wanted to camo and overmold the same stock. That proved to be easier said than done. Masking the overmolded part makes a horrible mess and overmolding directly over camo (without our process) has big adhesion problems. We experimented for a long time before coming up with a process that worked. We overmold over camo day-in and day-out without any problem. It looks great and holds up as well as direct overmolding applications”.
Craig Dougherty, PIM’s Marketing Director, echoed Ryan’s comments. “The ultimate added value is to decorate with camo and overmold the grip areas with a complementary color. We’ve done a lot of basic black over camo but overmolded tan, grey and green grips really punch it up. Now that our technology is protected, we expect to be doing more variations”. For more info, visit the PIM website at www.gunvalleymolders.com.
In the future, Virginians will enjoy the restored freedom to purchase multiple handguns within a 30-day period. The Commonwealth is repealing provisions of § 18.2-308.2:2 of the Code of Virginia restricting handgun purchases to one-a-month. After passing the Virginia Senate (21-19), legislation (HB940, SB323) overturning Virginia’s present one-handgun-a-month restriction is now on its way to the desk of Virginia Governor Bob McDonnell. As Gov. McDonnell has said he will sign this legislation into law, we can expect the one-gun restriction to soon be a thing of the past in the Commonwealth of Virginia.
“We are pleased that the Virginia Senate and House of Delegates have recognized the importance of repealing one-gun-a-month, legislation that rationed the Second Amendment rights of law-abiding Virginians,” said NSSF Senior Vice President and General Counsel Lawrence G. Keane. “We look forward to Gov. McDonnell’s signature on this very important bill.”
There was a lot of buzz at the Defiance Machine booth at SHOT Show. The new Defiance actions are beautifully made, and they have already been used in some impressive custom rifle builds. Defiance, based in Columbia Falls, MT, has rolled out a line-up of four (4) custom actions: Rebel, Mutant (for tubeguns), Renegade (for .408 CheyTac), and Titan (for 50 BMG). These actions all feature beautiful machining, with Wire EDM-cut lug ways, advanced-design extractors, and a true one-piece bolt. All action materials are pre-hardened before machining to prevent changing tolerances during heat-treating. Southpaws will be happy that both right and left-hand versions of all four actions are offered.
The Rebel actions feature a Remington 700 footprint for ease of inletting and stock compatibility. Notably, the Rebel actions are available in four lengths. Buyers can choose Medium, X-Medium, Long, or X-Long lengths to accommodate all popular factory chamberings and extended-length handloads. Multiple magazine well cuts are available for all of today’s popular magazine types including hinged floorplates, DBMs, or single-shot. For a rock-solid optics installation, Defiance can supply Mil-spec Picatinny rails with various built-in MOA geometry. This stout rail is secured to the action with five pins and 1/4-28 X 1/2″ screws. Base price on a Rebel is $1270.00 (Medium) or $1300.00 (Long), with many available extra-cost options. Defiance says delivery will take at least 60 days from order date.
We were very intrigued by the Mutant action with its integrated recoil lug. Offered in Medium and Long action lengths, Defiance’s new Mutant receiver is made specifically for the Eliseo RTM and RTS Chassis Systems. The Mutant features an extended tenon length for increased barrel thread contact and bedding surface. (Extended tenon is optional on the Rebel). The Mutant’s integral recoil lug adds rigidity and simplifies tubegun assembly. Medium-action Mutants are typically built with a Guardian mag-well cut to accommodate AI and AW magazines, while Long-action Mutants fit AI single-stack magazines and can be of Badger length or the longer CIP length for extended-OAL cartridge loading. The starting price on a Mutant action is $1200.00 (before options), and delivery is at least 60 days out.
The beefy Titan (50 BMG) and Renegade (.408 CheyTac) actions look like they will become very popular with the big-caliber shooters. These jumbo actions share the advanced features of their smaller cousins, but they are sized up significantly to provide additional strength, stiffness, and bedding surface. On both big actions double-plunger ejectors are used in combination with M16 extractors for reliable case ejection. Both Titan and Renegade actions are offered either as a single-shot or repeater. The Titan is currently sold exclusively through Proof Research, while the Renegade is not yet in production. Defiance plans to build 600 Renegade actions later this year, after demand is filled for the Rebels and Mutants. The anticipated price for the Renegade is $1750.00.
OK, we suspect we’ve whet your appetite. For final pricing (with customer-ordered options) and availability call Defiance at (406) 756-2727. For specs, features, and lots more photos, visit DefianceMachine.com. Contact Proof Research, 406-756-9290, with order questions about the 50 BMG Titan action.


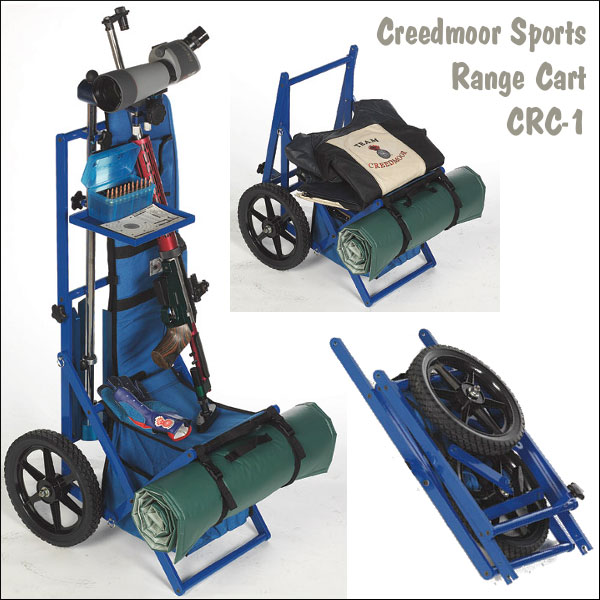 Some High Power shooters on the Forum asked about carts for carrying their gear to the range. You can certainly purchase a factory-made, purpose-built cart that folds up and has all the bells and whistles. The
 Check out the
 You’ll want to enclose the sides of the bottom box area so small items don’t fall out. You can tack-weld aluminum side-plates if you want a fancy appearance. I prefer to just cut sheet plastic from a home improvement store. These plastic panels can be attached with screws or even zip-ties around tubing.

 Past F-Open Class National Champion (and Forum Member) Larry Bartholome, has authored an authoritative article on the 2011 F-Class National Championship held last fall in Lodi, Wisconsin. Larry writes: “With a wind tunnel for a range, and rain that canceled the final team match, only the strongest stood on the winners’ podium when the Championships ended”. Larry provides a day-by-day guide to the match, with complete results for both F-Open and F-TR classes. You’ll find Larry’s article in the

 In addition, this month’s edition features a well-written, 4-page


 The NRA Competitive Shooting Department is promoting a trivia contest on its


 Turn Necks in a Single Pass

 Why does the 21st Century Neck-Turning Tool cut so well? First, the Neck-Turning Tool employs ultra-sharp carbide cutters that are custom-ground to fit the shoulder angle of your cartridge. This allows you to make a perfect cut extending down the shoulder 1/32 of an inch. Second, the system aligns the case neck on the arbor (mandrel) so well, and the cutter is so sharp, that very little torque is required. This allows the cutting process to go very smoothly. The case-holder is also unique — it features a O-ring so it holds the case firmly in place without marring or bending the case head. The tailstock case-holder adjusts to accommodate cases from 17 Fireball to a .416 Rigby.
 Applying overmolding to a decorated gunstock (camo, wood grain, etc.) has proven to be extremely difficult and costly and has not been practiced widely. As a result, overmolded stocks typically have a black, grey, tan or other basic, out-of-the-mold colors. See, e.g. the
 In the future, Virginians will enjoy the restored freedom to purchase multiple handguns within a 30-day period. The Commonwealth is repealing provisions of § 18.2-308.2:2 of the Code of Virginia restricting handgun purchases to one-a-month. After passing the Virginia Senate (21-19), legislation (


