New York, the state that brought suit to dissolve the NRA, has lost yet another important gun business. Firearms maker Kimber Manufacturing Inc. (Kimber) is leaving New York and heading south to Alabama. The primary reasons for the move are the anti-gun policies of New York, high state corporate taxes, and high costs of living for New York-based workers. Put together, New York had become a hostile environment for Kimber so it is moving to Alabama. Good riddance, New York.
Kimber is an American company that designs and manufactures firearms for individual, sporting, law enforcement, and military markets. Known primarily today for its handguns, Kimber also makes hunting rifles. In fact Kimber got its start building .22 LR sporting rifles. Kimber was originally founded as “Kimber of Oregon” in 1979 by Jack Warne and son Greg Warne in the small town of Clackamas, Oregon. It went through several ownership changes before relocating to New York and New Jersey.* Now Kimber will get a new start in Alabama.
Kimber issued this press release about its Relocation:
Kimber Mfg. is pleased to name Troy, Alabama, as its official corporate headquarters and to announce it is hiring aggressively in all departments. After a carefully planned shift of leadership, R&D and manufacturing resources, Kimber has made substantial progress in the transition to its new, state-of-the-art headquarters in Troy, Alabama. [The facility is] situated on 80+ acres with more than 225,000 square feet of space and is now home to industry-leading design engineering, product management, and manufacturing capabilities.
After an exhaustive search, Troy was chosen for a multitude of reasons including its proximity to top-tier engineering schools as well as gun- and business-friendly support from the city of Troy and the great state of Alabama. Kimber’s Alabama expansion is well ahead of schedule, having filled hundreds of its planned Troy-based positions.
Kimber Is Hiring Employees in Alabama
Kimber is seeking qualified applicants including CNC technicians, machinists, quality control specialists, design engineers, compliance analysts, customer service representatives, materials planners, maintenance technicians, finishing operators, and assembly technicians. Interested job applicants can CLICK HERE.
“Kimber is a great place to work, especially if you love firearms,” said Pedi Gega, director of assembly and product finishing. “We have two indoor gun ranges, one outdoor range, a state-of-the-art design and prototype fabrication center, and a dynamic team of professionals who pride themselves in producing firearms with unmatched attention to detail, design and performance.”
* An Australian, Jack Warne moved to Oregon in 1968 after Portland-based Omark Industries purchased the Australian firearms manufacturer, Sporting Arms (Sportco), he had founded in South Australia. Following its founding in 1979 by Warne, Kimber of Oregon built a reputation for .22 LR rimfire rifles, and then Kimber expanded to produce excellent centerfire rifles. After some setbacks, Kimber of Oregon filed for bankruptcy. In 1990, several Kimber employees, including Dan Cooper, left to found Cooper Firearms of Montana. But then in the mid-1990s, Greg Warne revived Kimber with the help of Les Edelman. The two founded Kimber of America. Edelman was also involved in New York-based Jerico Precision Manufacturing, which produced tools and mechanical components for the defense industry. Edelman combined Jerico Precision’s existing manufacturing capabilities and Kimber’s network of dealers to sell a line of M1911-style handguns. He eventually moved Kimber’s production line to Jerico’s facilities in New York, ending Kimber’s presence in Oregon. The company now will move from New York to Troy, Alabama.
Craters may look interesting on the moon, but you don’t want to see them on your primers. Certain mechanical issues that cause primer craters can also cause primer piercing — a serious safety problem that needs to be addressed. If you have a gun that is cratering primers (even at moderate pressure levels), there is a solution that works with many rifles — send your bolt to Greg Tannel to have the firing pin hole bushed.
Shooters who convert factory actions to run 6BRs, 6PPCs or other high-pressure cartridges should consider having the firing pin bushed. These modern cartridges like to run at high pressures. When running stout loads, you can get cratering caused by primer flow around the firing pin hole in the bolt face. The reason is a little complicated, but basically the larger the hole, the less hydraulic pressure is required to crater the primer.
A limited amount of cratering is normally not a big issue, but you can reduce the problem significantly by having a smith fit a bushing in the firing pin hole. In addition to reduced cratering, bushing the firing pin often produces more consistent ignition.
This is a highly recommended procedure that our editors have had done to their own rifles. Greg Tannel (Gre-Tan Rifles) is an expert at this procedure, and he does excellent work on a wide variety of bolts. Current price for a bushing job, which includes turning the firing pin to .062″, is $92.00, or $100.00 with USPS Priority Mail return shipping.
If you have a factory rifle, a bushed firing pin is the way to go if you are shooting the high-pressure cartridges such as 6PPC, 6BR, 6-6.5×47 and 6.5×47. This is one of the most cost-effective and beneficial upgrades you can do to your factory rifle. For more info on the Firing Pin Bushing process, visit GreTanRifles.com, or email greg [at] gretanrifles.com. After clicking the link for GreTanRifles.com, Click on “Services” > “Shop Services” and you’ll see a listing for “Bush Firing Pin Hole & Turn Pin”. CLICK that Box.
Firing Pin Hole Bushing by Greg Tannel
Work Done: Bush firing pin hole and turn pin
Functions: Fixes your cratering and piercing problems
Price: $92.00 + $8.00 return shipping Total Price: $100.00
Actions for which Bushing is Offered: Remington, Winchester, Savage multi-piece pin, Sako, Kimber, Nesika, Stiller, BAT Machine, Kelbly, Lawton, Surgeon, Borden, Wichita, Hall, Ruger, Howa, Weatherby, Dakota, Pacific Tool, Phoenix, and Defiant bolt action rifle or pistol.
Actions for which Bushing is NOT Available: Case hardened receivers, ARs, Accuracy International (AI), Barnard, Big Horn, Cooper, Desert Tactical Arms, Kimber, Rosenthal, New Savage single piece pin, Rim fires, Falling block, Break open, Lever, Pump rifles, 1903-A3, CZ, Mauser.
How to send your bolt in to be bushed:
Send your bolt and firing pin assembly via snail mail, priority mail, or UPS. Please do not use FEDEX as it sometimes has delivery delays.Include your name, phone number, and return shipping address, and a note as to what you want done. Pack your bolt carefully and ship to: Gre’-Tan Rifles, 24005 Hwy. 13, Rifle CO 81650.
Due to the high volume of work, turn-around time for bolt bushing jobs can be 12 weeks (though it usually is faster). Customers can pay by check, money order, or credit card. For more information visit GretanRifles.com.
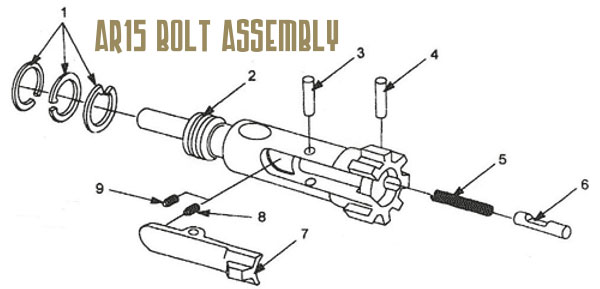
AR-platform rifles can be maintenance-intensive beasts. But some AR owners make the situation worse by not regularly cleaning important small parts, or by using too much oily/greasy lubricants in the wrong places. A properly maintained and lubricated AR15 can shoot hundreds of rounds (between cleanings) without a problem. If you learn where (and where not) to apply lubricant, you’ll find that your AR will run more reliably and the task of cleaning the bolt and bolt carrier will be less of a burden.
Here is a good video that explains AR-15 Cleaning and Maintenance. In this 30-minute NSSF video, Gunsite Academy instructor and gunsmith Cory Trapp discusses the proper way to clean and maintain the AR-15 carbine. Very knowledgeable, Trapp provides rock-solid advice for AR owners. Along with cleaning procedures, this video explains how to inspect key components and how to function-test your AR before each shooting session.
If you want to keep your black rifle running smoothly and reliably, you must clean it regularly and follow the correct maintenance procedures. Here’s another good video that explains how to properly disassemble and clean AR-platform rifles.
Take-Down and Full Cleaning of AR15 by Jerry Miculek
Here ace shooter Jerry Miculek takes down and cleans an AR-platform rifle belonging to his daughter Lena. This is a good video because Lena’s rifle was “run hard and packed up dirty” so you can see where carbon and grease build up. This 35-minute video is very thorough. Jerry is one of the nation’s top action carbine shooters, so listen carefully to his advice on cleaning and lubrication.
This video from Brownells talks about a the crown of a barrel and how the crown’s condition affects accuracy. As the bullet leaves the barrel of the gun, the shape, alignment and the condition of the crown can affect the accuracy of your shot. A proper crown is essential to ensure that the bullet leaves the barrel correctly and that the propellant gasses behind the bullet are distributed evenly on firing. A square crown without burrs and a smooth transition will normally ensure consistency from shot to shot. By contrast, a damaged crown can cause unpredictable flyers that open your group. That’s why it’s important to have perfect crowns on all your barrels.
The video explains the different types of crowns that can be used. In addition, the video shows how you can chamfer your muzzle in a home shop. If you use a properly-sized pilot, cutting a shallow chamfer is something that most guys with some mechanical skill can handle. Just be sure to use lubricant, flush chips, and don’t rush the job. Cutting the barrel is another matter. At the 1:20 mark the video shows how to use a hack-saw to remove a damaged muzzle section. While this may be fine for an inexpensive rifle that needs a “quick fix”, we do NOT recommend using a hack-saw with a vise for a competition barrel. The reason is that it is too easy for a novice to produce a cut that is not square. We suggest letting a professional gunsmith cut and crown your competition barrels.
As posted in the Calguns.net a few years back, there was a nasty out-of-battery firing incident involving a BOHICA Arms .510 DTC AR15 upper. The cause of the out-of-battery firing is not certain but it appears that the ammo was not sized properly and the firing pin may have been stuck in the extended position. As a result, the round went off before the bolt was closed with the lugs seated. In the process, the bolt handle broke off, as the bolt retracted violently, actually ending up outside the bolt raceway.
The shooter was badly injured, with broken bones and ligament damage to his left hand and tissue damage to his right hand. The shooter was holding the rifle with his left hand near the front of the chamber where a gas vent was located. Gas and shrapnel existed the vent hole causing the severe injuries to the left hand.
From range reports, it appears that the shooter had been struggling to chamber previous rounds, and was having trouble closing the bolt. After talking with one of the rangemasters, a poster on AR15.com reported: “The guy was using new reloads that weren’t exactly fitting well into his chamber. [The shooter] was slamming the bolt handle with his palm trying to get the cases to lock in. The guy was also slamming the bolt forward full force from the rearmost position back and forth trying to ram the cases into chamber in an attempt to squeeze the rounds in so the bolt could close. Finally, on one of the attempts … the possibly stuck firing pin rams into the primer and explodes the round when he slams the bolt forward (zero lug engagement hence the KB) and shooter puts himself into a world of hurt.”
Lessons Learned — Don’t Try to Force Oversize Ammo into a Chamber
By all reports, the shooter’s ammo wasn’t fitting his chamber properly. In an effort to force the ammo into the chamber, he worked the bolt with excessive force. That MAY have caused the firing pin to extend or the hammer to fall without the trigger being pulled. One theory is that the trigger system may have been modified, allowing the hammer to fall from the force of slamming the bolt forward. Others have speculated that the firing pin may have failed to retract because the bolt handle was over-torqued — a safety issue listed in the BOHICA manual.
Whatever caused the out-of-battery firing, it appears that improperly-sized ammo (or a poorly-cut chamber) was the root cause of the problems. If you go to a range and find your bolt does not close easily over the ammo — STOP SHOOTING — don’t try to force the issue. Disaster may result. To paraphrase Johnnie Cochran: “If the ammo doesn’t fit, it’s time to quit”.
Photos by Wildcard, originally posted on Calguns.net.
Jim Borden of Borden Accuracy/Borden Rifles is adding “something extra” to the Borden actions crafted for F-Class Team USA members. These actions feature a Team Name and Team shield thanks to modern computer-controlled laser engraving. Jim Borden posted: “Here is Tony at Endless Laser Art doing his thing. [Team members] James Crofts, Drew Rutherford, Dan Bramley, Keith Trapp here we come!”
Jim is crafting special actions for both the F-TR and F-Open Team USA squads with laser-engraved USA F-Class Team shields. There is a BRMXD-type called USA Open and a BRM-type action called USA FTR. The F-Open serial numbers start USAFOPEN01 while F-TR numbers start USAFTR01. These are offered to members of USA F-Class Teams.
Watch Laser Engraving of Borden Actions
Watch the video above to see U.S. Rifle Team shield laser-engraved on Borden actions for F-Class Team USA and F-TR Team USA.
Don’t Tread on Me — Laser-Engraved Ax Blade for NRL Founder
Here’s a another example of modern, computer-controlled laser engraving. Travis Ishida, one of the founders of the NRL Precision Tactical series, has obtained a laser engraving machine. This can be great for putting identifying marks on tools, metal gunstocks, motorcycle parts — basically anything where you want some words and/or graphics. We like the message Travis printed on his Ax: “Liberty or Death… Don’t Tread on Me”. Travis posted: “Finally got my laser engraver working and now I want to engrave everything in sight! This could be a lot of fun… and a little obsessive.”
For this Sunday GunDay article we feature a “blast from the past” — David Tubb’s engineering tour de force, the Tubb 2000, or “T2K” for short. With the remarkable T2K, David earned multiple NRA High Power championships, and David shot the first-ever perfect score in the NRA Long-Range “any sights” championship 16 years ago.
Our write-up this week focuses mostly on “hardware” because David’s performance with the rifle speaks for itself. He has won eleven High Power National Championships at Camp Perry, and in 2004 David mounted a scope to his rifle and captured the Long-Range “any sights” Championship with a 1450/1450, the first and only perfect score ever logged at Camp Perry. He did this all with his trusty 6XC-chambered T2K, shooting the DTAC 115gr bullet in a 1:7.5″-twist Schneider P5 barrel. For more information about this remarkable competition rifle, read on.
[Editor’s NOTE: Because this is an article from our older Archives, some technical details may have changed with time. For all current specifications on TUBB rifles, including the TUBB 2000, visit DavidTubb.com. For more information on the particular T2K rifle featured in this story, CLICK HERE.]
Mag-Feed Action with Unique Bi-Camming Bolt
The action is machined from 17-4 stainless steel to true benchrest quality standards. The design features a solid top with a loading port. This increases action stability, stiffness, and strength. The loading port is easily accessible and is angled to aid the shooter in single loading rounds. The Tubb 2000 is fed via 10- or 20-round box magazines.
“I prefer using 20-round magazines with the Tubb 2000 because it provides a secure hand hold when shooting off the bipod. For across the course competition, the 10-round magazines are the best choice as they do not encumber sling-supported shooting positions. There is no difference in the functioning or reliability of either capacity magazine.”
One-finger Bolt Operation
Low effort bolt operation was a key goal in the design of the Tubb 2000 action. The exclusive bi-camming design employs two cams that engage during bolt lift to radically reduce bolt lift effort. Bolt lift is 75 degrees. The cone-faced bolt has two locking lugs which are narrower and taller than on conventional actions. This design allows the magazine to be mounted higher in the action for smoother, more positive feeding. The bolt handle is designed for superior performance in sustained fire operation. Its ergonomic shape allows operation with a single finger, if desired. The bolt is machined from 8620 carbon steel and rides back into the butt extension, under the shooter’s face so the bolt can be operated without the shooter having to change his head position. This low center of gravity also improves the rifle’s feel and performance under recoil.
The action features a full-length Picatinny rail that will accept Weaver®-style mounts. The action’s adjustable sight mounting system allows the rail to be mounted at one of three pre-set mounting angles — 0, 5, and 10 degrees — to allow the shooter to level the sights to fit his shooting style. A custom base is available to mount match iron sights. All barrels have a small section at the muzzle turned down to accept a clamping-style front sight mount or cant indicator.
The T2K’s Lock Time is ONE millisecond — over three times faster than a Model 70 Winchester.
Barrel Configuration
Tubb 2000 rifles featured hand-lapped stainless steel match barrels with the exclusive “Tubb Contour.” This unique contour maximizes accuracy and minimizes weight — it’s the perfect balance. According to David: “It’s a contour where the barrel wouldn’t shoot one bit better if it was one bit bigger.” The Tubb 2000 was conceived as a “switch barrel” gun — it’s designed to be easily re-barreled by the customer. This feature means that the same rifle can support different calibers and shooting disciplines. Finished barrels in a variety of calibers were available for “do-it-yourself” installations. The gun shown here has a Schneider barrel.
The Tubb 2000 has, over the years, been offered in a variety of chamberings including: .22-250; .243 Winchester; 6mmBR Norma (6BR); 6XC; .260 Remington; 7mm-08; and .308 Winchester. Available accessories include finished barrels, extra 10- or 20-round magazines, cleaning rod guide, adjustable bipods, custom adjustable handstop, fore-end weight rail, and cant indicator.
Trigger, Stock Adjustment and Other Features
The Tubb 2000 uses the superb Anschütz® fully-adjustable two-stage trigger (with safety); one of the finest available to the precision rifleman. This trigger can also be adjusted to provide single-stage operation. The buttstock assembly, forend, buttstock clamping block, and magazine housing, trigger guard assembly are made from 60-series aluminum, hard anodized in the customer’s choice of 6 colors: light and dark teal, purple, red, forest green, and black. (The T2K Tactical (see below) comes in matte black only.) These four parts are each available in any of the listed colors, allowing the purchaser to design his own distinct rifle.
The buttstock is FULLY adjustable for length, height, cant (angle), and offset. The cheekpiece is adjustable for height. An easily accessible knurled wheel allows the shooter to adjust the cheekpiece from the shooting position. Shooter comfort is further augmented by an ergonomic pistol grip. All adjustment features on the Tubb 2000 were designed for easy shooter access. The butt extension, clamping block, shock housing, and buttplate all have index marks to allow the shooter to record and repeat adjustment settings. The tubular fore-end can be rotated and positioned to accommodate the shooter’s preference. An integral accessory rail accepts a custom adjustable handstop or bipod. The fore-end also incorporates a built-in barrel heat wave blocking system which eliminates optical distortion in the sighting plane.”
David Tubb Explains T2K Stock Adjustments
I advocate setting stock length a little longer than most people might. I am a firm believer that it is best to “reach” slightly for the pistol grip as this ensures a strong, secure hold on the rifle. I pull the rifle firmly into my shoulder pocket when shooting offhand, and also prefer to have what I would characterize as very firm contact between rifle butt and shoulder in the sitting and prone positions as well. When using a sling in prone or sitting, stock length (and sling tension) should be great enough so that, at the least, you have to push the buttpad forward with your hand in order to place the stock into the shoulder pocket. My buttstock is shortest offhand and longest prone. If my standing setting is “0”, I’m usually out about 1-1/2 inches for sitting and about another inch for prone. I have found that many people tend to shoot with a stock that’s too long in sitting and too short everywhere else.
I have found the cast off/on adjustment feature on the buttstock to be of great help to me in attaining the natural shooting positions I desire. For prone, I offset the clamping block so the buttplate moves outward [the index mark on the clamp is to the right of center on the scale on the receiver extension tube]. I swing it a little bit inward for offhand and slightly more inward for sitting. The amounts of cast on/off (in clock-face terms) are approximately 6:30 for standing, 4:30 for prone, and 8:00 o’clock for sitting.
Stock Length Adjustment Procedure
The buttstock is adjustable in length 4+ inches. This adjustment is accomplished by moving the buttplate tube in or out after loosening the four screws on the clamping block. Ensure that the buttstock tube is fully contained in the block. The extent of rearward (lengthening) movement is determined by the front of the buttstock tube fitting flush with the front of the block.
Stock Cast and Cant Adjustment Procedure
The buttstock is adjustable for cast or offset by loosening the four screws on the clamping block and swiveling the block on the receiver extension tube. The buttplate itself is adjustable for cant up to 360 degrees and after loosening the screw directly in the center of the rubber recoil pad is adjustable for height at approximately 1-1/2 inches. The cheekpiece is adjustable vertically approximately one inch. The vertical cheekpiece adjustment is accomplished via the top knurled ring. The lower knurled ring will then secure the setting.
About David Tubb — Tubb 2000 Designer
David Tubb is arguably the winningest centerfire rifleman in history. He has won a record eleven NRA National High Power Rifle Championship titles at Camp Perry, along with six NRA Long Range HP Championships. In addition, David is an NRA Silhouette Rifle legend, having won nearly 30 open, individual National Championship titles in all four rifle categories. David has also won seven Sportsmen’s Team Challenge Championships and multiple Wimbledon Cups. His latest big win was the 2019 NRA ELR Championship in Heavy Gun Class.
For more information on the
Tubb 2000 Rifle contact:
David Tubb Accuracy
and Precision Gun Parts
800 N. 2nd Street
Canadian, TX 79014 DavidTubb.com
Phone: (806) 323-9488
If two barrels are better than one, then why not three? That’s the thinking behind the exotic Bockdriling BD14 from Blaser, unveiled at the 2014 IWA Show in Germany. This three-barrel Bockdrilling firearm works as a shotgun, large-caliber rifle, and small-caliber rifle all in one. Even with all those barrels, the BD14 is relatively light, at 3.3 kg (7.26 lbs) without optics. That makes this a nice, carry-around gun for stalking. As you’d expect from Blaser, the twin triggers are crisp and precise, with a pull weight of just 1.43 lbs (650 grams). The front trigger is for the large-caliber rifle barrel, while the rear trigger works both the shotgun and small-caliber barrels, via a tang-mounted selector. These firearms are rare in the USA — and quite expensive. The only Blaser BD 14 we could find on GunBroker had a $9099.95 asking price. That works out to over three grand per barrel.
Here’s what Blaser USA has to say about its unique three-barreled BD 14:
“The ‘Bockdrilling’ is, put simply, an over/under (O/U) rifle-shotgun combination with a smaller caliber rifle-barrel… on the side. The barrel arrangement [allows] for an extremely slender receiver, making the BD14 exceptionally huntable.
The [patent-pending] Vertical Block Lockup… combines an extremely compact and solid block lockup in a closed system within the monoblock with the comfortable handling of a classic break-action rifle.
The double lock permits, if needed, a rapid second shot, the front trigger always releasing the large rifle-caliber. The … barrel selector actives the shotgun barrel when in position ‘top’ and activates the smaller rifle caliber in position ‘bottom’.”
Why Does Anyone Need Three Barrels?
The Blaser website explains: “As hunters, we learn to expect the unexpected, whether in a blind or stalking, so it’s understandable that we dream of a firearm that will allow us to take advantage of any situation. With the Bockdrilling BD14, Blaser has developed the perfect blind and stalking firearm – compromises are finally a thing of the past.”
Design Features of the Bockdrilling BD 14 Tri-Barrel Gun
The BD14 has a double-lock system so that a second shot can be taken without having to recock the firearm. Blaser says: “Thanks to the free-floating barrels, point of impact remains constant even with a quick succession of shots, no matter which barrel was fired first. The extremely strong vertical block lock on the BD14 helps contribute to the high degree of precision.”
Story idea from EdLongrange. We welcome reader submissions.
We have used NO-LEAD Cleaner in rimfire benchrest rifles similar to this modified Suhl 150-1. It helped restore accuracy with minimal brushing.
Made by the same smart folks that created Wipe-Out™, and Carb-Out™, NO-LEAD Brushless Lead Remover™ really works. Honest. If you are an active rimfire shooter, or if you shoot cast lead-alloy bullets in centerfire rifles and pistols, you should try this product. We now use NO-LEAD in our rimfire benchrest rifles, and in some centerfire guns that receive a steady diet of soft-alloy cast bullets (90%+ lead). (With rimfire guns, you don’t need to use NO-LEAD very often — maybe every 300-400 rounds unless you have a real fouler of a barrel.)
If you’ve got stubborn lead fouling in a rimfire barrel, or on a pistol’s muzzle brake/compensator, you should definitely give this stuff a try. We don’t know how but it does soften lead deposits. The manufacturer says you don’t need brushes, but we found that a bit of brushing (after NO-LEAD application) can help remove more serious lead build-up.
Yes we were surprised to find a lead remover that really works. We tried a half-dozen other lead “cleaners” that promised to dissolve lead and most of them, we discovered, are nearly useless. There’s a reason for that, as the lead alloys used in bullets don’t react to typical petrochemical-based solvents. It took the Wipe-Out chemists over five years to perfect this water-based solution that really does dissolve lead.
NO-LEAD Cleaning Procedure — Read Carefully NO-LEAD Lead Remover is a clear, red gel that is easy to apply. Just swab it in your bore (or on muzzle brakes) with wet patches or bore mop and let it sit for a few minutes. (The manufacturer says you can leave the NO-LEAD for up to 20 minutes, but that long of a dwell time does not seem necessary with our rimfire barrels.) When it contacts lead it will start to foam and you’ll see that the NO-LEAD solvent turns a pastel pink when it dissolves lead. The pink comes from the formation of lead oxide. After the recommended dwell time, simply patch out the dissolved lead deposits (you can also use a nylon brush for stubborn lead build-up).
NOTE: After cleaning, it is very important that you get all the NO-LEAD out of your barrel, and neutralize it. We recommend following the application of NO-Lead with Wipe-out or Patch-Out to neutralize the NO-LEAD, clear the bore, and remove residual carbon and copper fouling. If you don’t have Wipe-Out or Patch-out, flush the barrel thoroughly with Rubbing Alcohol or even a solution of Dawn dish detergent — then re-oil the bore.
Be Sure to Neutralize NO-LEAD After Use
Remember that N0-LEAD is a strong, slightly acidic chemical that needs to be neutralized after use. If you leave it on a nice, blued barrel for too long, it can harm the bluing. NO-LEAD will remove all the surface oils from the barrel bore. For this reason it is recommended that you neutralize NO-LEAD with Wipe-Out, or Patch-Out, which both contain effective corrosion inhibitors. If you don’t have those products, once you’ve flushed the NO-LEAD with something like rubbing alcohol, then follow with a gun oil. Caution: A petroleum-based gun oil will NOT, by itself, neutralize NO-LEAD. You need to neutralize first, then apply the corrosion inhibitor (or do it all in one step with Wipe-Out or Patch-Out).
Where to Buy NO-LEAD Lead Remover
NO-LEAD Lead Remover costs $16.99 for an 8 oz. squeeze bottle with a flip-top spout. This product is sold directly by Sharp Shoot-R Precision Products through Sharpshootr.com, or you can purchase NO-LEAD through many other online vendors. For more information, send an email via the Sharp Shoot-R Contact Form or or contact SharpShoot-R at (785) 883-4444. You can ask for Terry Paul, Sharp Shoot-R’s owner and the master chemist who developed the NO-LEAD formula.
Here is what high-end hunters have been requesting for years — an ultra-lightweight mag-fed action with Benchrest-grade smoothness, engineering, and craftsmanship. BAT Machine has just introduced two impressive new aluminum/steel hybrid repeater actions — the Bumblebee (short action) and the Vampire (long action). These are REALLY light. BAT states 23.8 ounces for the Bumblebee, and Alex Wheeler reports the Vampire is 25.3 ounces. So you get titanium-class weight savings without the titanium hassles.
Both the Bumblebee ($1699 MSRP) and the Vampire ($1765 MSRP) are aluminum/steel designs with integral recoil lugs and +20 MOA Picatinny rail segments. Though they are flat-bottom actions, both are designed to fit most Remington 700-pattern stocks. Gunsmith Alex Wheeler says: “This action shape should be very stable in the bedding — you just need to square up the inlet.”
Both the Vampire and Bumblebee actions feature a modular bolt. BAT does the modular bolt differently than anyone else, and very cleverly. This design allows easier bolt face changes and spring changes. Internal maintenance is also easier. Bat bolts also run super smoothly. Alex Wheeler reports “the Vampire action is very smooth — it feels just like BAT’s all-steel actions.”
Vampire action photos courtesy WheelerAccuracy.com. The Vampire fits a 4″-long CFE-09 magazine box.
Alex Wheeler got one of the first Vampire actions, and he was impressed. This is a long-action repeater, with standard or Magnum bolt. Alex says the mating of steel and aluminum was superb: “I have checked it for straightness and lug contact. It’s very good. I’m impressed with how straight they got this insert.”
Bumblebee Action — State-of-the-Art Lightweight Hunting Action
If you are seeking a very lightweight action with Benchrest-quality smoothness and precision fit/finish, consider the Bumblebee. Weighing under 24 ounces, this new Bumblebee short action may be perfect for hunters, varminters, and tactical shooters who desire a light weight, premium quality action. The new Bumblebee is designed to use 700 Short Action bottom metal. Combining steel and aluminum, the Bumblebee combines 4140 Chromoly Steel and 7076-T6 Aluminum to achieve strength and rigidity at a weight rivaling titanium. According to BAT, the Bumblebee’s advance design makes it “31%-42% stiffer than light weight steel actions and over 130% stiffer than round Titanium actions.”
Bumblebee Action Features and Specifications:
— Action weight is 23.8 oz. as configured in photos (11.4 oz. lighter than BAT VR/TR actions)
— Weight comparable to Titanium actions after including Picatinny rails, recoil lugs, and fasteners
— 31%-42% stiffer than lightweight steel actions and over 130% stiffer than round Titanium actions
— Action body made with aircraft-grade billet 7075-T6 Aluminum and hardened 4140 Chromoly Steel
— Integral +20 MOA Picatinny two-section rail standard
— Modular bolt for lower cost bolt face changes
— .070″ firing pin diameter for maximum accuracy and reliable ignition
— Standard medium aluminum bolt knob, 5/16-24 thread
— LiFe Melonite-treated firing pin, bolt and shroud for smooth bolt movement and low maintenance
— Extended extraction cam for smooth bolt opening
— Uses Remington 700 SA trigger components and bottom metal
— Right-hand and left-hand versions
— Barrel tenon is 1.062 x 18 tpi (CLICK HERE for blueprint)
Product tip from EdLongRange. We welcome reader submissions.


 Craters may look interesting on the moon, but you don’t want to see them on your primers. Certain mechanical issues that cause primer craters can also cause primer piercing — a serious safety problem that needs to be addressed. If you have a gun that is cratering primers (even at moderate pressure levels), there is a solution that works with many rifles — send your bolt to
 Firing Pin Hole Bushing by Greg Tannel



 Jim Borden of


 Trigger, Stock Adjustment and Other Features


 Stock Cast and Cant Adjustment Procedure


 Made by the same smart folks that created Wipe-Out™, and Carb-Out™,
 Where to Buy NO-LEAD Lead Remover


